Non magnetic fasteners should be selected against a defined magnetic-performance requirement, not simply a stainless-steel label or an informal magnet check. Alloy, metallurgical condition, forming, machining and the completed assembly can affect the result. For an instrument or electrical product, first identify the sensitive component, relevant field conditions and acceptable disturbance. Then specify the finished fastener’s material, geometry and verification method alongside its mechanical and corrosion requirements. A screw that appears weakly attracted to a handheld magnet is not automatically unsuitable, while a screw that shows no obvious attraction has not automatically passed a quantitative permeability requirement.
Start with the function being protected. A nearby magnetic sensor, precision instrument or other field-sensitive component may respond to a fastener differently from a general enclosure. Distance, orientation and the operating field can matter. Give the supplier a measurable requirement or an approved qualification procedure instead of expecting the phrase “non-magnetic” to describe every acceptable condition.
Distinguish material permeability from an assembled product’s performance. Permeability describes a material’s response to a magnetic field under stated conditions. Remanent magnetization and the influence of neighboring parts are different questions. The responsible designer should identify which property or system response controls acceptance; a single attraction demonstration does not answer them all.
Record where the requirement applies. It may cover the whole fastener, a critical region near a sensor, or every part of a supplied kit. Nuts, washers, inserts, coatings and nearby structural members should not disappear from the review. Replacing only the screw can leave another component responsible for the assembly’s unwanted response.
Stainless steels comprise different metallurgical families. Their magnetic behavior cannot be inferred from corrosion resistance or surface brightness alone. The Australian Stainless Steel Development Association’s technical explanation distinguishes those families and explains how processing can alter the response of austenitic stainless steel. Use a named alloy and delivered condition rather than a generic stainless designation.
Cold working can change the response of some austenitic grades. A fastener’s head, thread and shank may experience different forming histories. Consequently, a property measured on incoming wire does not necessarily describe every location on the finished screw. This is a reason to define the specimen and measurement location, not a reason to reject every formed stainless part.
A2 or A4 identification also should not replace a magnetic acceptance criterion. Those fastener material groups support a different specification purpose. If magnetic response is critical, request evidence relevant to the exact alloy, condition and finished configuration. Keep that evidence separate from strength-class and corrosion documentation.
Austenitic stainless steel may be considered where corrosion and mechanical requirements also suit the application. Other candidate families can include copper alloys, aluminum alloys, titanium alloys or nonmetallic materials. Each requires its own assessment of strength, stiffness, temperature, corrosion, conductivity, creep and manufacturing constraints. Low magnetic response does not make two materials mechanically interchangeable.
Replacing a steel part with another material may require changes to thread engagement, bearing area or installation limits. The mating material and joint load path remain important. Do not reuse a steel torque value merely because the replacement has the same nominal thread size. Engineering should approve the completed configuration and installation process.
Availability is another boundary. A manufacturer’s photo of a stainless screw is not evidence that every listed candidate alloy is offered, qualified or suitable. Ask the supplier to confirm the requested material and process capability for the drawing. This guide identifies selection questions; it does not assign unverified magnetic ratings to TNHO products.
| Requirement | Definition to supply | Evidence to request | Common mistake |
|---|---|---|---|
| Application response | Sensitive feature and relevant field or operating condition | Approved component or assembly evaluation | Treating all instruments as equivalent |
| Material | Alloy, condition and permitted substitutions | Traceable material and processing records | Ordering only “stainless” |
| Magnetic acceptance | Property, method, location and acceptance rule | Results linked to the specified specimen | Using attraction as a numerical rating |
| Joint performance | Loads, environment, engagement and installation | Engineering review and relevant qualification | Copying a different material’s torque |
| Production control | Lot identity, sampling and change-control requirements | Delivered-lot documentation | Accepting an unrelated catalog statement |
The checklist deliberately contains no universal permeability limit, sampling count or installation value. Those requirements belong to the application specification and the selected measurement procedure.
ASTM A342/A342M-26 addresses procedures for evaluating permeability of weakly magnetic materials. Its scope and specimen restrictions matter. Do not assume that a procedure suited to semifinished material can be applied unchanged to a small, irregular finished fastener. Agree on the method and specimen suitability with the laboratory.
Define the relevant field condition, test region and specimen preparation through the adopted procedure. If the instrument or fixture requires a particular geometry, explain how that requirement is met. A result from a specially prepared sample should remain identified as such; it must not silently become a measurement on the shipped screw.
Keep units, instrument identity, verification status and the acceptance decision with the report. Results close to a limit need an appropriate uncertainty and decision-rule review. The NIST guidance on measurement uncertainty supports clear evaluation and reporting; it does not set a magnetic limit for an unspecified product.

A handheld magnet can reveal an obvious difference during an investigation, but the observation depends on the magnet, separation, specimen size and handling. It is not automatically a calibrated permeability test. Decide whether such a check is permitted for identification, screening or another limited purpose, and document its limitations.
If a purchaser and supplier disagree about an attraction observation, preserve the samples and identify the conditions used by each party. Compare the part number, lot, measurement location and preparation. Escalate to the agreed method rather than strengthening the magnet or changing the test until the preferred outcome appears.
Do not equate attraction with wrong alloy. A processing-related response can require investigation even when chemistry is correct. Conversely, chemistry alone may not establish the finished part’s required magnetic behavior. Material identification and performance verification answer different questions and should be reviewed together.
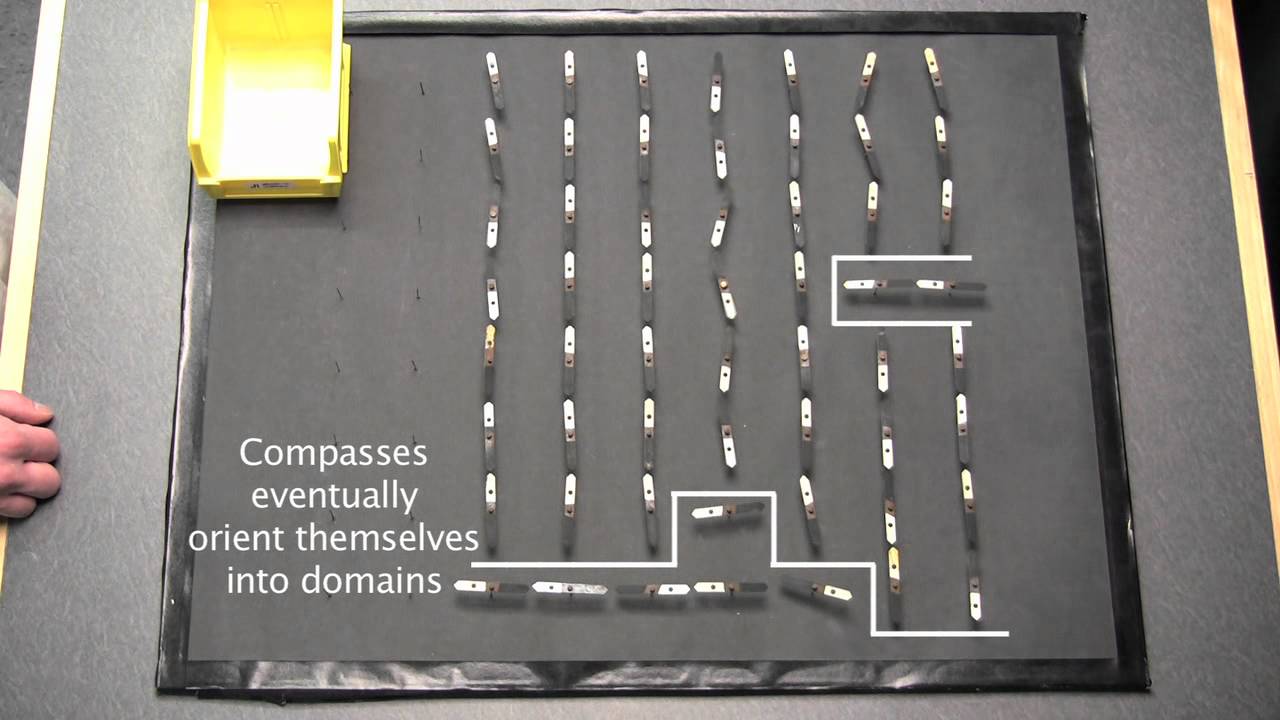
The MIT Physics Instructional Resources Lab demonstrates magnetic-domain behavior using interacting compass needles. The analogy helps explain why internal organization matters to magnetic response. It is not a stainless-fastener test and supplies no acceptance value for a screw.
Qualification should identify the exact configuration, processing route and evaluated condition. Decide which changes require renewed review, such as a material substitution, forming route or finishing change. A favorable result from a prototype should not authorize an undocumented production alternative with different geometry or history.
Receiving inspection should follow the agreed sampling and documentation rules. Preserve individual results and identify nonconforming specimens rather than reporting only a lot average. Where a complete assembly is qualified, maintain the supporting parts and installation configuration as well. An approved fastener may perform differently after an uncontrolled assembly change.
TNHO’s combination-drive screw family illustrates one relevant geometry. The A2 and A4 guide provides material-group context, while the material-certificate guide and lot-traceability guide help organize purchasing evidence. None substitutes for the agreed magnetic verification.

At receiving, reconcile the purchase-order requirement with the report before approving the shipment. Check whether the sample is finished hardware or source material, whether its identity matches the supplied drawing revision, and whether the measurement covered the specified region. If a report uses a different condition or procedure, request an explanation rather than recording a generic “pass.” The disposition should identify exactly which requirement the evidence supports.
Preserve the original sample-selection record when parts from several manufacturing lots are packed together. A test on one convenient specimen does not automatically represent every bag or finishing batch. Define how sample IDs relate to the shipment and keep rejected or questioned results visible. Where the plan permits additional testing, document why it was requested and how the final decision relates to the original result.
For an assembly-level investigation, compare a controlled baseline with the proposed fastener configuration under the same operating conditions. Keep component position, instrument setup and supporting hardware unchanged unless the test explicitly evaluates them. Record unintended differences so that a change in system response is not attributed to the screw alone. This comparison is an application-specific verification step, not a universal magnetic-material test.
No. Alloy family and delivered metallurgical condition matter, and processing can affect the response. Specify the required property and verification.
No. Investigate material identity and processing history separately from magnetic performance, using the agreed methods.
Only within an approved evidence scope. Forming and geometry may require finished-part evaluation or additional qualification.
Include the drawing, alloy and condition, application boundary, magnetic method and criterion, mechanical requirements, sampling and traceability.

 TNHO