Shoulder screw tolerance determines whether a shoulder screw can locate, guide, or pivot a component without excessive play, binding, or rapid wear. The key is not to choose the tightest possible fit. The designer must define the actual function, then coordinate shoulder diameter, mating-hole diameter, shoulder length, head and underhead geometry, thread runout, surface finish, coating, lubrication, temperature, and alignment. A fit that rotates freely in a clean laboratory can seize after plating, contamination, or thermal expansion, while too much clearance can produce impact loading and inaccurate motion.
A shoulder screw combines a head, a precision or semi-precision unthreaded shoulder, and a smaller threaded section. The shoulder diameter controls radial fit with the mating bore. Shoulder length controls the distance between the head bearing face and the step near the thread. The step and thread runout need relief so the mating part can sit on the intended shoulder rather than an incomplete thread. Head thickness, head diameter, drive, and underhead fillet affect tool access, seating, and local clearance.
Do not assume every product sold as a shoulder screw has the same tolerance system. Standard products may follow an established inch or metric standard, while custom step screws follow a controlled drawing. The ASME catalog page for ASME B18.3 identifies a key standard family for socket cap, shoulder, and set screws. Confirm the required edition, product type, and exact tables before placing dimensions on a drawing.

A clearance fit leaves the bore larger than the shoulder throughout the permitted tolerance range. It is normally required for free rotation or sliding, but the amount of clearance controls play, lubricant film, contamination tolerance, and impact. A transition fit can produce either small clearance or small interference and is generally used for accurate location where free motion is not guaranteed. An interference fit intentionally makes the shaft larger than the bore over at least part of the tolerance range; it is not a routine choice for a removable rotating shoulder screw.
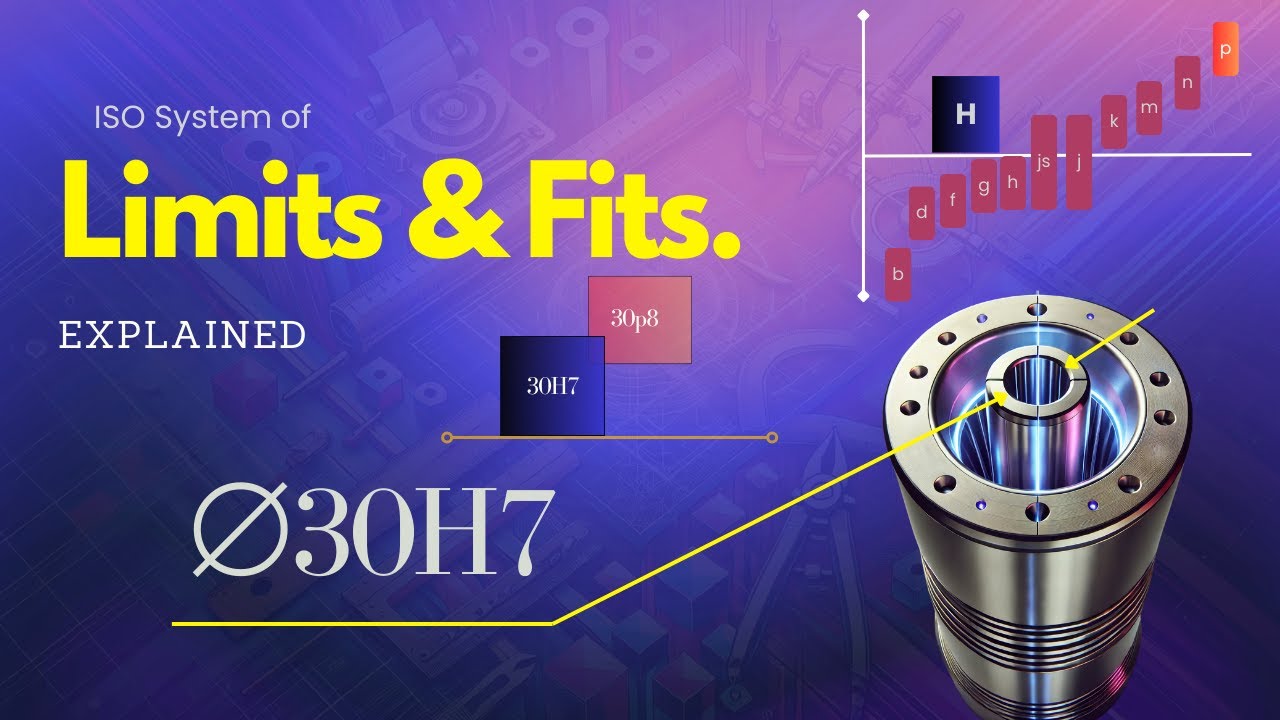
The ISO system of limits and fits provides standardized tolerance zones through ISO 286-1 and related documents. A designation is meaningful only when the nominal size range and the tolerance zone for both hole and shaft are known. Never copy a fit callout from an unrelated diameter or material without checking the current standard and the manufacturing process.
| Assembly function | Fit direction | Main risks | Drawing and validation focus |
|---|---|---|---|
| Free pivot with bushing | Controlled clearance | Binding, wear, noise, impact, lubricant loss | Shoulder and bore limits, roundness, finish, lubrication, side load, temperature |
| Sliding guide or stop | Clearance matched to contamination and alignment | Jamming, galling, accumulated positional error | Straightness, bore alignment, edge breaks, debris allowance, coating thickness |
| Accurate removable location | Close clearance or transition after engineering review | Difficult assembly, fretting, loss of repeatability | Datum structure, true position, mating-part process capability, service removal |
| Fixed pin function | Transition or interference may be considered | Cracked hub, high press force, distortion | Material strength, wall thickness, lead-in, press method, retention and removal |
| Low-cost noncritical hinge | Generous clearance | Rattle and uneven bearing | Maximum acceptable play, wear life, washer or spacer control |
The table intentionally avoids universal numeric clearances. Suitable limits depend on nominal size, load, speed, materials, manufacturing capability, and service environment. Use a recognized fit system or a validated custom tolerance analysis.
For a simple cylindrical pair, minimum diametral clearance equals the minimum bore diameter minus the maximum shoulder diameter. Maximum diametral clearance equals the maximum bore diameter minus the minimum shoulder diameter. A negative result indicates interference. This arithmetic is simple, but the inputs must include the size after all finishing operations and at the relevant temperature.
Diametral clearance is not the whole motion error. Radial movement is approximately half the diametral clearance for a centered cylindrical pair, and angular play increases with shorter bearing length. Position error also includes bore location, perpendicularity, cylindricity, shoulder straightness, head seating, bracket flexibility, and wear. In a multi-link mechanism, stack these contributors using the project’s approved worst-case or statistical method.
Temperature can change clearance when shoulder and housing materials have different thermal expansion. The change in a dimension is approximately the original dimension multiplied by the material’s expansion coefficient and temperature change. Use verified material data and the actual operating range; do not use a room-temperature fit as proof of hot or cold performance.
Shoulder length is often overlooked because designers focus on diameter. If the shoulder is shorter than the moving member or bushing stack, tightening the screw can clamp the moving part and prevent rotation. If it is much longer, axial play can create noise, impact, or poor location. The step must project through the moving stack enough for the threaded end or support face to tighten without pinching the pivot.
Calculate minimum and maximum axial clearance using shoulder-length limits and the complete mating stack. Include washers, bushings, coatings, compressed seals, and production tolerances. Confirm that the head’s underface seats on the stationary member intended by the design. A generous fillet or thread runout can create false seating if the mating hole lacks a compatible chamfer or relief.
Diameter tolerance alone does not guarantee a durable bearing. Roughness peaks can raise friction and wear. A soft shoulder running directly in a hard abrasive bore can wear rapidly; two similar stainless surfaces may gall without suitable material pairing or lubrication. Black oxide, zinc plating, nickel plating, and other finishes add different thicknesses and change friction and corrosion behavior. The drawing should state whether the dimensional limits apply before or after coating.
For a rotating joint, define whether the shoulder turns inside the bushing or remains fixed while the bushing rotates around it. That choice affects which surfaces need controlled finish and lubrication. Specify environmental restrictions on lubricant, such as food contact, vacuum, dust, or temperature, and validate service intervals.
This independent educational video explains the purpose of limits and fits. It supports the selection method here but does not provide a product-specific tolerance.
A size tolerance controls local diameter but does not fully control the shoulder axis relative to the thread or head. If the screw is a precision locator, consider runout, straightness, perpendicularity, and coaxiality or position requirements appropriate to the datum scheme. Apply only controls that the function needs and that the supplier can measure reliably.
The NIST/SEMATECH Engineering Statistics Handbook provides general resources for measurement and process analysis. A practical inspection plan identifies the instrument, contact points, temperature, coating condition, sample size, and calibration status. A micrometer can check accessible shoulder diameter, but it cannot by itself prove axis alignment, cylindricity, or functional fit across the full bearing length.

Functional gauges can be useful in production when designed from approved limits, but they should not conceal the cause of rejection. For first articles and process changes, record actual measurement data and review capability near tolerance boundaries.
The shoulder may carry lateral load, but the thread retains the screw and supports clamp or reaction forces. Specify thread size, pitch, class, engagement, and tightening method. The support material must provide adequate thread strength. Avoid bottoming the screw in a blind hole before the intended face seats. If a locking patch, adhesive, prevailing feature, or jam nut is used, qualify it for service temperature, chemicals, reuse, and maintenance.
The shoulder-to-thread step is a stress transition. Sharp geometry, side loading, bending, and cyclic impact can produce fatigue. Review the complete load path and use the applicable calculation method and safety factor. For related selection principles, see the thread engagement guide and the screw length tolerance guide.
Provide a dimensioned drawing with clear datums and define shoulder diameter and limits, shoulder length and limits, thread, head geometry, drive or wrenching feature, underhead fillet, step relief, end form, material, heat treatment or hardness, finish, surface texture where functional, and whether dimensions apply before or after coating. Add inspection, documentation, traceability, packaging, and cleanliness requirements.
Also provide application information: mating bore limits and material, bushing type, radial and axial load, motion angle and frequency, speed, temperature, corrosion environment, lubrication, desired service life, and acceptable play. That context helps identify contradictions before tooling. TNHO’s custom step shoulder screw page shows the relevant product family; actual geometry and properties remain quotation- and drawing-specific. The partial versus full thread bolt guide provides a complementary comparison for ordinary bolted joints.
Prototype with production-intent materials, finishes, bores, bushings, and lubrication. Check assembly force, starting torque, running torque, radial play, axial play, temperature rise, wear debris, noise, and loosening under the representative load cycle. Inspect both the shoulder and bore after testing. A mechanism that merely moves by hand at assembly has not demonstrated service life.
During production, monitor the dimensions that drive minimum and maximum clearance and the processes most likely to drift. Coating changes, tool wear, heat-treatment distortion, and supplier substitutions require review. Keep the drawing, control plan, inspection method, and functional test aligned.
There is no universal value. Choose clearance from nominal size, desired play, bearing length, load, speed, materials, finish, lubricant, contamination, temperature, and manufacturing capability. Calculate both minimum and maximum clearance using the specified limits.
Not automatically. A rotating or sliding joint normally needs positive clearance under all allowed conditions. A transition or interference relationship may suit a fixed locating function, but it can prevent motion or damage a thin hub if applied without analysis.
Yes, deposited coating changes the finished size. The drawing should say whether diameter limits apply before or after coating, and the supplier should control the process accordingly. Validate fit using fully finished production-representative parts.
Use calibrated equipment suited to the tolerance and feature: micrometers or air gauges for diameter, appropriate methods for length and finish, and alignment measurement when required. Define temperature, coating condition, datums, sampling, and acceptance rules on the inspection plan.

 TNHO