Thread Inserts For Metal selection is not just a matter of matching a name in a catalog. It is a replaceable internal thread installed in a drilled, tapped, cast, or formed metal hole. For an OEM buyer, the reliable approach is to connect the fastener geometry to the joint function, installation process, service environment, and inspection plan.
This guide explains how the part works, the main variations, what must appear on a drawing or RFQ, and which failures should be checked before production approval. It is written for engineers, sourcing teams, and quality staff comparing standard and custom industrial fasteners.

The insert increases the effective thread engagement area and can restore a stripped hole or create a durable female thread in a soft parent metal. That working principle is more useful than the product name alone because two parts with similar catalog descriptions may behave differently when the parent material, contact surface, or installation method changes.
Common applications include aluminum housings, machine-tool fixtures, transportation castings, maintenance repair of stripped threads. In every case, the fastener is part of a joint system. The surrounding material, hole preparation, mating thread, driver, applied torque or press force, and exposure conditions determine whether it performs consistently.
Do not select a type solely from a photograph. Confirm the functional feature on a dimensioned drawing and ask whether the supplier controls that feature during production. A sample that looks correct can still have an unsuitable thread fit, hardness, coating thickness, or working geometry.
| Input | What to define | Who should confirm it |
|---|---|---|
| parent alloy and hardness | State the drawing value, tolerance, test method, and acceptance rule. | Supplier engineering and buyer quality team |
| internal thread and tolerance class | State the drawing value, tolerance, test method, and acceptance rule. | Supplier engineering and buyer quality team |
| external installation thread or hole size | State the drawing value, tolerance, test method, and acceptance rule. | Supplier engineering and buyer quality team |
| installed length and minimum wall thickness | State the drawing value, tolerance, test method, and acceptance rule. | Supplier engineering and buyer quality team |
| installation tool, locking feature, and surface finish | State the drawing value, tolerance, test method, and acceptance rule. | Supplier engineering and buyer quality team |
Use one dimensional system consistently. Reference a current recognized standard when a standard part truly satisfies the design, but add application-specific requirements separately. For a custom part, identify inspection datums and avoid tolerances that are tighter than the joint needs; unnecessary precision raises cost and can obscure the characteristics that actually protect function.
Material choice must account for mechanical load, wear, temperature, corrosion, conductivity, and interaction with the mating components. Carbon or alloy steel often supports higher strength and predictable heat treatment. Stainless steel improves corrosion resistance but can gall in threaded contact. Brass, aluminum, and engineered polymers serve specialized electrical, weight, or corrosion needs.
A finish is not merely a color. Zinc systems, nickel, black oxide, passivation, and proprietary coatings differ in corrosion performance, friction, thickness, and electrical behavior. Specify the coating system and acceptance requirement rather than requesting a vague color. Check whether coating buildup can alter thread fit or working dimensions.

Typical problems include incorrect mating geometry, cross-threading, insufficient engagement, surface damage, loss of clamp load, rotation, pull-out, corrosion, and driver damage. The relevant failure depends on the mechanism: a locking feature must retain resistance, a sealing interface must maintain controlled compression, and a precision shoulder or bearing surface must preserve alignment.
When a failure appears, do not automatically increase torque. Excess torque may strip a parent thread, distort sheet metal, crush a seal, damage a drive, or overload a narrow bearing surface. Separate the possible causes—part geometry, incoming material, installation, and service load—and reproduce the issue with controlled samples.
Incoming inspection should confirm identity, critical dimensions, thread acceptance, material or hardness evidence, finish, and visible defects. Functional testing then verifies the feature that matters in the actual joint. Depending on the product, this may include prevailing torque, push-out, torque-out, pull-out, leakage, clamp load, rotation resistance, or repeated assembly testing.
Agree on the sampling plan and measurement method before mass production. A measurement without a stated datum, instrument, conditioning rule, or pass/fail threshold is difficult to reproduce between buyer and supplier. Retain approved samples and link inspection records to the lot.

Before releasing the drawing, ask what the joint must do if friction changes, the mating material arrives at its tolerance limit, or the assembler uses the highest permitted installation setting. Review access for the driver or press, the direction of service load, nearby edges, and the space needed for tools and inspection. For this product family, pay particular attention to parent alloy and hardness, internal thread and tolerance class, and external installation thread or hole size. These inputs should be confirmed together rather than assigned independently.
Next, define the boundary between a catalog characteristic and an application requirement. A supplier can certify the fastener material, dimensions, and finish, but the buyer normally owns the mating component, stack-up, and service load. Use representative mating parts for approval testing. If production parts come from multiple tools or vendors, include samples from the expected extremes instead of validating only a nominal prototype.
Finally, decide how a change will be controlled. Tool replacement, raw-material source, heat-treatment route, coating supplier, lubricant, or packaging can affect assembly even when the part number stays the same. List the changes that require notification and renewed approval. This is especially important when the joint relies on friction, deformation, penetration, sealing compression, or a close dimensional fit.
Ask whether the supplier manufactures this product family regularly, which operations are performed in-house, and how tooling and special processes are controlled. Review measurement capability for the critical geometry and request realistic evidence: material certificates, coating reports, first-article results, capability data, and traceable functional tests.
For custom work, send annual demand, batch size, target delivery, packaging, and approval expectations with the drawing. This lets the manufacturer select a sensible process instead of pricing an undefined risk. TNHO supplies related custom fastener products and can review geometry, materials, finishes, samples, and inspection requirements before production.
Use applicable product standards and the drawing as the controlling purchase documents. The ISO fastener technical committee and the ASME B18 fastener standards program explain the scope of widely used dimensional standards. For joint fundamentals, Bolt Science provides an independent overview of bolted-joint behavior. Always verify the edition and applicability required by your drawing, customer, and market.
Complete inputs shorten quotation time and reduce assumptions. If a dimension is unknown, state the joint function and provide mating-part information rather than inventing a value. A capable supplier can then propose a controlled option for engineering approval.
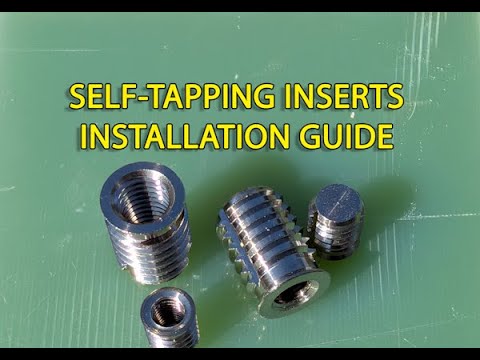
Thread Inserts For Metal is a replaceable internal thread installed in a drilled, tapped, cast, or formed metal hole. The name identifies a useful geometry or locking function, but a purchase specification must still define dimensions, material, finish, and verification.
Start with the joint function and service environment. Then confirm parent alloy and hardness, internal thread and tolerance class, and external installation thread or hole size. Validate the final choice in the real assembly.
Reuse depends on the locking or sealing mechanism, thread condition, installation history, and the governing engineering rule. Do not assume reuse is acceptable merely because the part can be removed.
Include a drawing or recognized standard, parent alloy and hardness, internal thread and tolerance class, external installation thread or hole size, material and finish, order quantity, inspection level, packaging, and any required sample approval.
Thread Inserts For Metal performs reliably when its geometry, mating interface, material, finish, installation, and verification method are specified as one system. Begin with the joint function, select the appropriate type, validate it in representative parts, and preserve the approved requirements in the drawing and control plan. For adjacent design considerations, see our related fastener engineering guide or send TNHO your drawing for a manufacturability review.

 TNHO


